- This topic is empty.
-
AuthorPosts
-
2026-10-15 at 6:19 pm #9882
Image Source: https://www.xuxiangtaimetal.com How does Qingdao Xuxiangtai ensure your custom metal orders meet US quality standards? Our comprehensive, multi-stage inspection system delivers the answer. We designed this system to address your primary concerns: reliability, consistency, and compliance. From raw material testing to final packaging, we verify every step. You receive exactly what you ordered, when you need it.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Key Takeaways
- A multi-stage inspection system catches defects early, saving you from costly returns and delays.
- In-house quality engineers provide faster feedback and more accurate reporting than third-party inspectors.
- Complete documentation, including material certificates and test results, ensures smooth US customs clearance.
Why a Complete Quality Inspection System Matters for US Buyers
The Real Cost of Quality Failures in Overseas Sourcing
A single defective batch can derail your entire production schedule. You face return shipping costs, replacement manufacturing delays, and potential downtime on your assembly line. Worse, a failed component in the field could trigger liability claims or damage your reputation with end customers. These hidden costs often exceed the original purchase price by several times. You need a partner who prevents these scenarios before they happen.
How Full-Chain ISO Quality Control Builds Trust
Working with a fabrication company that adheres to strict global production standards required for ISO certification gives you assurance that your large structural parts will be reliable and error-free. Defective parts can result in product error and breakdown, causing potential lawsuits and costly delays. By preventing these defects through ISO-certified processes, businesses save time and money, directly reducing the defect rate in the supply chain.
Raw materials and components directly affect the quality of finished products. ISO 9001 requires manufacturers to evaluate and select suppliers based on defined criteria, verify incoming materials against specifications, and monitor supplier performance over time. This is one of the most impactful areas of the standard for manufacturers because poor incoming material quality is a leading root cause of production defects.
When you choose Qingdao Xuxiangtai, you gain a partner whose quality system covers every link from raw material testing to final packaging. You receive documented proof at each stage, not just promises. This transparency builds lasting trust between your team and ours.
The Advantage of In-House vs. Outsourced Inspection
Third-party inspection adds cost, scheduling complexity, and communication gaps. Our in-house quality engineers work directly with production staff. They catch issues immediately, not after parts ship. You receive faster feedback loops and more accurate reporting. This integrated approach means fewer surprises and smoother project execution.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Stage 1: Raw Material Testing and Pre-Production Verification
Every successful custom metal order begins with rigorous raw material testing and pre-production verification. This first stage protects your investment before a single part enters manufacturing. You need certainty that the metal arriving at our facility meets your specifications. You need assurance that the final product will perform reliably in its intended application. Our Stage 1 inspection protocol delivers both.
Spectral Analysis for Material Integrity
The foundation of any quality metal component lies in its chemical composition. A slight deviation in alloy percentages can compromise strength, corrosion resistance, or weldability. You cannot afford to discover these issues after production begins. That is why we perform spectral analysis on every incoming material batch before we cut, cast, or machine anything.
Optical Emission Spectrometry (OES) stands as our primary verification method. This technique detects over 34 elemental contaminants and provides complete chemistry analysis for both stainless steel and aluminum alloys. OES measures elements that other methods cannot detect, including carbon content—the most critical alloy ingredient in stainless steels. Carbon controls hardness, strength, weldability, and brittleness. Differentiating between L grade (<0.03% carbon) and H grade (≥0.03% carbon) stainless steels requires precise carbon measurement. Our OES equipment delivers this accuracy.
For aluminum fabrications, we follow ASTM E3061-17 standard test methods. This protocol evaluates products against The Aluminum Association’s composition limits. We verify mechanical properties and chemical composition through Material Test Reports (MTRs) that document every batch’s specifications.
Method Elements Detected in Stainless Steel Elements Detected in Aluminum Alloys Limitation XRF Iron, chromium, nickel, molybdenum Magnesium, silicon, copper, zinc, manganese Cannot verify carbon content; may require another method to separate grades differing in carbon OES More complete chemistry; measures elements XRF cannot More complete chemistry; measures elements XRF cannot Requires surface preparation and leaves a small burn mark We also employ handheld LIBS (Laser-Induced Breakdown Spectroscopy) analyzers for field verification. These portable devices rapidly determine major and minor alloy elements across a wide concentration range. This capability proves essential for Positive Material Identification (PMI). Using the wrong grade can lead to economic loss or even catastrophic failure—such as explosions in chemical plants. Our technicians verify material grades on-site, in real time, without waiting for laboratory results.
For stainless steel fabrications, our testing protocol includes:
- Corrosion testing
- Eddy-current or ultrasonic testing
- Hardness measurement
- Spectrochemical analysis
- Melt and heat-trace verification
- Microstructure examination
- Surface finish inspection
- Tensile and yield testing
Each test confirms a specific property. Together, they provide complete assurance that your material meets ASME/ASTM standards. We validate Material Test Reports against actual material properties. We verify heat numbers and material grades for full traceability. You receive documented proof that every component originates from certified material.
Supplier and Subcontractor Audits
Your supply chain extends beyond our facility. We source raw materials from vetted mills and foundries. We partner with specialized subcontractors for certain processes. Each link in this chain must meet the same quality standards we hold internally.
Our procurement team conducts regular audits of every material supplier. We evaluate their production capabilities, quality systems, and track records. We verify their certifications and inspect their facilities. We maintain approved supplier lists that require ongoing performance monitoring. A supplier who fails to meet our criteria loses approval status immediately.
For subcontractors, we apply the same rigorous standards. Whether they handle heat treatment, surface coating, or specialized welding, we audit their processes. We review their equipment calibration records. We inspect their quality documentation. We require them to adhere to our inspection protocols and reporting standards.
This comprehensive approach ensures that no weak link compromises your order. You receive components manufactured entirely within a controlled quality ecosystem. Every supplier and subcontractor understands your requirements because we communicate them clearly and verify compliance at every step.
Engineering Drawing Review and DFM Validation
Before production begins, our engineering team conducts a thorough review of your drawings. We examine every dimension, tolerance, and specification. We identify potential manufacturing challenges. We propose solutions that improve manufacturability without compromising your design intent.
Design for Manufacturing (DFM) validation represents a critical value-add. Our engineers analyze your design for production efficiency, material utilization, and structural integrity. They identify features that may prove difficult to machine or cast. They suggest alternative approaches that reduce cost and lead time while maintaining performance.
This review also confirms that your specifications align with US import requirements. For electrical hardware components, we verify whether UL or ETL listings are required. These certifications often come from buyers, electrical codes, or insurers rather than customs. Confirming these requirements before placing an order prevents costly delays and compliance issues.
We also prepare the complete documentation package required for US import:
Document Purpose Who Provides It Commercial Invoice Establishes transaction value for duty calculation Your Chinese supplier Packing List Details contents of each container or package Your Chinese supplier Bill of Lading (B/L) Shipping contract and receipt of goods Ocean carrier or freight forwarder Certificate of Origin Confirms country where goods were manufactured Supplier or Chinese Chamber of Commerce HTS Classification Determines applicable duty rates You or your customs broker Customs Bond Guarantees payment of duties and compliance Surety company through your broker Entry Summary (CBP Form 7501) Official import declaration to CBP You or your customs broker Arrival Notice Notifies you when cargo arrives at port Shipping line or freight forwarder Our team prepares these documents during the pre-production phase. You receive a complete package that streamlines customs clearance and eliminates surprises at the border.
The engineering review also establishes clear quality benchmarks. We document every critical dimension and tolerance. We define inspection checkpoints for the production phase. We create a quality plan that guides our team from first cut to final packaging. This plan becomes your roadmap to a defect-free delivery.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Stage 2: In-Process Inspection During Manufacturing
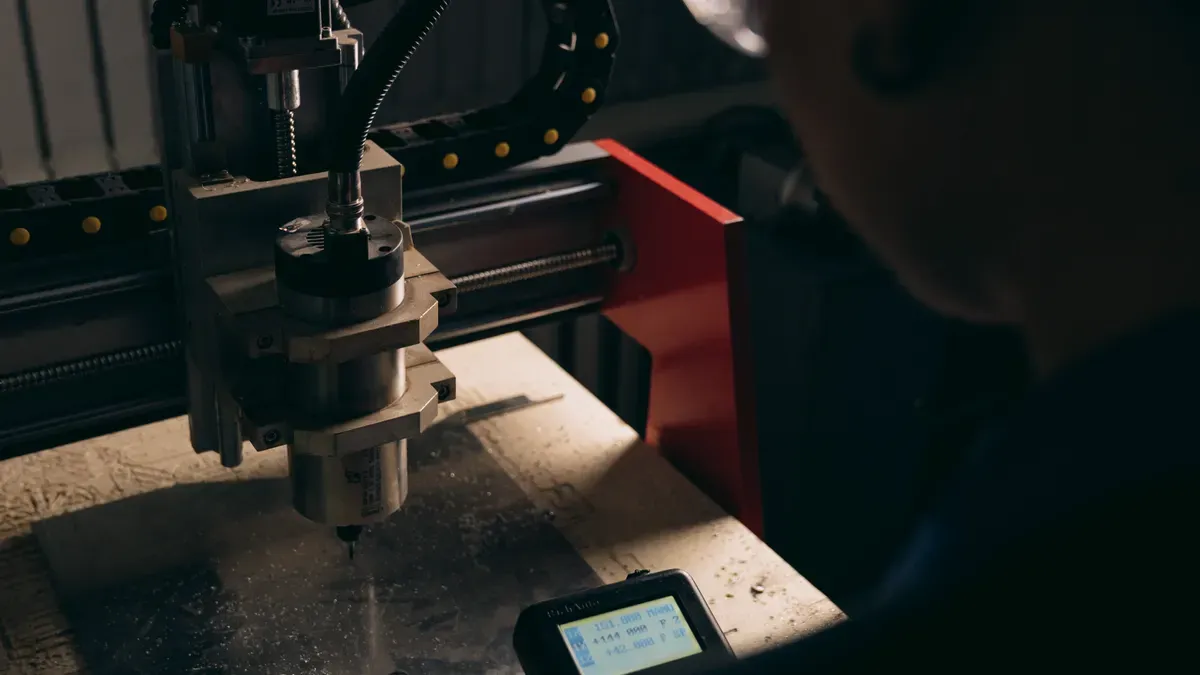
Image Source: https://www.xuxiangtaimetal.com Production begins only after your drawings pass our rigorous pre-production review. The second stage of our quality system now takes center stage. In-process inspection catches issues while we can still correct them quickly. You receive components that meet every specification because we verify each critical step during manufacturing, not after completion.
This stage directly addresses the concerns of US purchasing managers who need certainty about overseas metal manufacturing orders. You cannot afford to discover dimensional errors or weld defects after parts arrive at your facility. Our in-process inspection protocol eliminates that risk through systematic verification at defined checkpoints throughout the production cycle.
Dimensional Accuracy Checks at Critical Milestones
Dimensional accuracy determines whether your components fit together correctly in final assembly. A deviation of even a few thousandths of an inch can render a part useless. Our quality engineers perform dimensional inspections at multiple milestones during fabrication, not just at the end.
We use calibrated calipers, micrometers, coordinate measuring machines (CMMs), and precision gauges to verify tolerances against your engineering drawings. Each measurement gets documented and compared against the specified tolerance range. Any deviation triggers immediate corrective action before we proceed to the next manufacturing step.
The tolerance standards we apply depend on your specifications and target market. For US buyers, we typically reference ASME Y14.5 for geometric dimensioning and tolerancing (GD&T). This standard dominates North American manufacturing and provides detailed control frames for each feature. For general mechanical parts and weldments, ISO 2768 offers a simpler approach with blanket tolerances for untoleranced dimensions.
Aspect ISO 2768 ASME Y14.5 Approach General/blanket tolerances for untoleranced dimensions Symbolic GD&T per feature with individual control frames Philosophy Independence principle (each dimension checked separately) Envelope principle (Rule #1) ensuring perfect form at MMC Complexity Simple, one designation covers all Detailed, each feature requires its own specification Best for General mechanical parts, weldments, simple assemblies High-precision fits, aerospace, medical, complex assemblies Regional use Common in Europe, Asia, global supply chains Dominant in North America, US defense, automotive OEMs Default in CNC ISO 2768-mK (±0.1 to ±0.3 mm typical) No blanket default; tolerances must be specified per feature Your industry often determines which standard we apply. Automotive suppliers in the US require ASME Y14.5 as part of OEM supply chain specifications. Aerospace components demand ASME Y14.5 due to safety-critical tolerances on every feature. Medical devices may follow ISO 13485 with ISO 2768 for EU market compliance. Consumer electronics and general industrial parts typically use ISO 2768-mK as a cost-effective solution.
When manufacturing in China for export, the best practice is to specify both standards on the drawing, for example: “ISO 2768-mK unless individual tolerances per ASME Y14.5 are indicated.” This ensures clarity and compliance across different regional expectations.
Our engineers review your drawings to identify which standard applies. We then create a dimensional inspection plan that targets every critical feature. This plan guides our technicians through each measurement checkpoint. You receive documented results that confirm compliance with your specified tolerance requirements.
Welding Quality and Structural Integrity Testing
Welded joints often represent the weakest points in metal fabrications. A poorly executed weld can compromise structural integrity and lead to catastrophic failure under load. Our welding inspection protocol follows AWS D1.1 standards, the recognized benchmark for structural steel welding in North America.
We begin with qualified welding procedures for every joint configuration. Our welders hold certifications that match the specific processes and materials used in your order. We monitor heat input during welding to prevent metallurgical damage. We verify fit-up alignment before welding begins to ensure proper joint geometry.
Visual inspection serves as the first and most important verification step. Our inspectors examine every weld bead for surface defects, proper profile, and workmanship quality. They check for undercut, porosity, incomplete fusion, and excessive reinforcement. Any visual defect triggers immediate repair or rework.
Beyond visual examination, we apply non-destructive testing methods to verify internal integrity. The table below outlines the primary methods we use according to AWS D1.1 acceptance criteria.
AWS D1.1 Testing Method Purpose in Structural Integrity Verification Visual Testing (VT) Primary inspection step for surface defects and workmanship Ultrasonic Testing (UT) Volumetric examination for internal discontinuities Magnetic Particle Testing (MT) Surface and near-surface flaw detection in ferromagnetic materials Liquid Penetrant Testing (PT) Surface-breaking flaw detection in non-porous materials Ultrasonic testing uses high-frequency sound waves to detect internal discontinuities that visual inspection cannot reveal. This method proves essential for load-bearing structural components. Magnetic particle testing identifies surface and near-surface flaws in ferromagnetic materials. Liquid penetrant testing detects surface-breaking defects in non-porous materials. Each method provides specific information about weld quality and structural soundness.
Our inspection service aligns with AISC 360, AISC 341, and IBC provisions to ensure full compliance with US structural requirements. You receive test reports that document every weld inspection. These reports provide the traceability you need for quality audits and regulatory compliance.
Surface Finish and Coating Verification
Surface finish affects both the appearance and the corrosion resistance of your components. A rough surface can harbor moisture and contaminants, accelerating corrosion. An improperly applied coating can peel, chip, or fail to provide adequate protection. Our surface inspection protocol verifies both finish quality and coating performance.
We begin with visual inspection of surface texture and appearance. Our inspectors check for scratches, pits, burrs, and other surface defects. We measure surface roughness using profilometers to confirm compliance with your specified Ra values. We verify that machined surfaces meet your finish requirements before any coating application.
For coated components, we verify film thickness using calibrated gauges. The table below shows typical standards we apply for protective coatings.
Standard / Test Key Value / Requirement ASTM B117 (Salt Spray) E-coating: 500–1,000+ hours; AFP coating: up to 500 hours RoHS E-coating formulations are compliant REACH E-coating formulations are compliant ISO 12944 E-coating is compliant Film Thickness E-coating: 15–25 μm; AFP coating: 2–8 μm Environmental E-coating is water-based, near-zero VOC, ~100% transfer efficiency We offer multiple transit coating options to protect your components during ocean freight. Oil and solvent-based coatings create a thin molecular barrier against moisture and oxygen. Water-based coatings provide corrosion protection with low environmental impact and fast drying. Grease-based coatings deliver heavy-duty protection for harsh environments and extended storage periods.
Our coating verification process includes adhesion testing to ensure the coating bonds properly to the substrate. We perform salt spray testing according to ASTM B117 to validate corrosion resistance. We document all results in your inspection report, giving you confidence that your components will survive the journey across the Pacific and perform reliably in service.
The in-process inspection stage represents your best defense against manufacturing defects. We verify dimensional accuracy, weld integrity, and surface quality at every critical milestone. You receive components that meet your specifications exactly, without surprises at your receiving dock.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Stage 3: Pre-Shipment Inspection and Final Verification
The final stage of our quality system protects your investment when components are ready to leave our facility. Pre-shipment inspection verifies that every part meets your specifications before cargo loading. This stage catches any issues that might have escaped earlier checks. You receive complete confidence that your order arrives exactly as designed, documented, and ready for installation.
Final Assembly and Fit-Up Validation
Complex metal fabrications often require multiple components to fit together precisely at your facility. A dimensional error discovered during installation creates costly delays and forces expensive rework. Our pre-shipment protocol includes a full trial assembly of your complete order before we package anything.
We perform a 100% assembly of every mating part. We do not sample or spot-check. Every component gets connected to verify proper fit. This approach ensures that no mismatched parts slip through the process.
We use the actual hardware specified in your bill of materials during this trial assembly. The exact bolts, nuts, and washers you specified must pass through every hole without resistance. We do not allow hammering or forcing. If a fastener does not slide through cleanly, we identify the problem and correct it before shipping.
Match marking plays a critical role in this process. We label every connecting joint with clear identifiers. For example, “Joint A1 connects to A2” appears on both mating surfaces. These labels remain visible after packaging so your installation team knows exactly how each piece fits together.
We document the entire trial assembly with video. A continuous recording shows our technician inserting bolts by hand to prove perfect alignment. You receive this video with your inspection documentation. You can verify the fit-up quality without being present at our facility.
The table below outlines the specific validation checks we perform during final assembly:
Verification Point Success Criteria Common Failure Mode Bolt Hole Alignment Fasteners pass through all aligned holes without resistance or hammering. Drifting holes due to weld shrinkage. Planarity / Flatness Mating surfaces sit flush with no gaps exceeding the specified tolerance (e.g., <0.5mm). Warping from uneven heat distribution. Overall Envelope The assembled structure fits within the maximum defined L x W x H dimensions. Cumulative tolerance stack-up errors. Interference Check No moving parts or cable paths are obstructed by weld reinforcement or gussets. Weld spatter or oversized welds blocking clearance. Each verification point has a clear success criterion. We measure against these standards and document the results. Any failure triggers immediate corrective action before we proceed to packaging.
Export Packaging Standards and Protection
Ocean freight exposes your components to harsh conditions. Salt air, humidity, and physical shock can damage unprotected metal surfaces. Our packaging protocol follows international standards designed specifically for maritime transport.
For ocean voyages, export-ready crates can be equipped with vapor barriers, desiccants, and heat shrink wrap to keep moisture out. For high-value cargo, sealed crates and water-resistant coatings offer an additional layer of defense against humidity and salt damage.
We apply vapor-corrosion-inhibitor (VCI) packaging to all ferrous components. VCI materials release corrosion-inhibiting compounds that protect metal surfaces without direct contact. This technology prevents rust formation even in high-humidity environments.
Container desiccants absorb moisture that accumulates during temperature changes. The temperature swings between day and night on the open ocean create condensation inside sealed containers. Desiccants prevent this moisture from reaching your components.
We separate all metal-to-metal contact points with protective padding. Bare metal surfaces touching each other can cause abrasion damage during transit. We use foam padding and spacers to prevent scratching and fretting.
For precision-machined surfaces, we apply additional protection. The table below shows our packaging methods and their applications:
Packaging Method Purpose Best Use Case VCI Film/Paper Rust prevention Export shipments with long transit times Foam Padding & Spacers Scratch prevention Finished or precision-machined parts Coatings (spray/dip/peel) Moisture barrier Surface-critical items Desiccants + Sealed Bags Moisture control Humid climates or sea freight We also apply the IMO/ILO/UNECE CTU Code for cargo securing. This international code governs the safe packing of cargo transport units. Our logistics team verifies that all components are properly supported and secured within the crate. We confirm that coating protection remains intact and moisture risks are minimized.
For raw-wood packing materials, we verify ISPM 15 treatment and marking. This international standard prevents the spread of pests through wooden packaging. US Customs requires this certification for all wood packaging materials entering the country. We ensure your shipment complies before it reaches the port.
Documentation Review for Customs Compliance
Complete documentation prevents customs delays and ensures smooth entry into the United States. Our team prepares and reviews every required document before your shipment leaves our facility. You receive a comprehensive package that satisfies all regulatory requirements.
The pre-shipment inspection checklist guides our documentation review. We follow this systematic process:
- Surface and edge inspection: Check edges, connection areas, and handling damage; record approved repairs. Confirm protection of specified surfaces (e.g., bolted-joint contact areas) during transport, and agree on repair instructions and compatible materials for the receiving team.
- Packing list reconciliation: Obtain a package-level packing list linked to member marks, quantities, weights, and dimensions. Keep loose connection plates, braces, and fasteners identifiable. Coordinate shipment batches with the contractor’s erection sequence.
- Transport and packaging compliance: Review supports, securing, coating protection, and moisture risks with logistics personnel. Apply the IMO/ILO/UNECE CTU Code for cargo securing. For raw-wood packing, verify ISPM 15 treatment and marking per destination requirements.
- Release evidence pack: Prepare an indexed pack including: approved drawing register, material certificates, welding/NDT/dimensional/coating records, nonconformance reports with dispositions, piece-mark and packing lists, shipping photos, handling/storage/repair instructions, and release authorization.
- Reconciliation and release decisions: Use a reconciliation sheet to expose gaps (e.g., drawing revision mismatch). Explicitly decide: Release when evidence is complete; Hold when results are missing or discrepancies unresolved; Permit documented concessions only through authorized process. A shipping deadline must not close a nonconformance silently.
The core customs documents we prepare include the commercial invoice with correct Incoterms and HS codes, a detailed packing list, the bill of lading, and the VCCI-issued ordinary Certificate of Origin. We also submit the Importer Security Filing (ISF) at least 24 hours before vessel loading as required by US Customs and Border Protection.
Material and quality certificates accompany every shipment. Mill test certificates (MTCs) match to the exact heat number of the raw material used. First article inspection reports document initial production runs or drawing revisions. Certificates of conformance reference your purchase order number, drawing revision, and material specification. For tight-tolerance parts, we include CMM dimensional reports and surface finish or hardness reports.
Origin and tariff-related evidence receives special attention. The VCCI ordinary Certificate of Origin serves as the standard document CBP examines. Production records document the substantial transformation that occurs at our facility. MTCs trace raw steel to non-Chinese mills when necessary to avoid Section 301 tariffs. Our customs broker confirms whether Section 232 or Section 301 duties apply based on the HTS classification.
We also apply Acceptable Quality Limit (AQL) sampling according to ISO 2859-1 for final outgoing inspections. The standard defines AQL as the “quality level that is the worst tolerable,” representing the maximum number of defective units beyond which a batch is rejected. For most consumer goods, common limits are 0% for critical defects, 2.5% for major defects, and 4.0% for minor defects. For metal fabricated parts, the acceptable AQL must be defined by the buyer based on the product’s end use and risk level. Components used in building an airplane require much lower AQL limits than general industrial parts. We work with you to establish appropriate AQL levels for your specific application.
Our documentation review ensures every certificate, report, and form meets US import requirements. You receive a complete package that streamlines customs clearance and eliminates surprises at the border.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Aligning with US and International Quality Standards
Your components must meet rigorous standards before they enter the US market. We align our entire inspection system with the frameworks that US purchasing managers recognize and trust. This alignment protects your company from compliance failures, liability risks, and costly delays. You gain confidence knowing every component meets the same quality benchmarks whether it ships to Texas, Ohio, or California.
ASTM, ISO, and IATF 16949 Compliance
Quality standards form the backbone of our inspection protocols. We structure our processes around internationally recognized frameworks that US buyers and regulatory bodies accept without question. These standards govern everything from material composition to final documentation.
ISO 9001:2015 serves as our foundational quality management system. This standard requires us to evaluate suppliers, verify incoming materials, and monitor production processes continuously. We maintain certification through regular third-party audits. Our quality manual documents every procedure, from raw material receiving to final shipment release.
ASTM standards govern material testing and product specifications. We reference ASTM A967 for passivation of stainless steel components, ensuring corrosion-resistant surface layers form correctly. We apply ASTM B117 for salt spray testing of coated surfaces. These standards provide measurable acceptance criteria that our inspectors verify with calibrated equipment.
IATF 16949 extends beyond general quality management for automotive applications. This certification demands additional rigor in risk analysis, process control, and traceability. We maintain this qualification because many US automotive OEMs require it from their supply chain partners. Your components receive the same disciplined oversight whether they serve automotive, aerospace, or industrial applications.
The table below summarizes the key standards we apply to your orders:
Standard / Certification Status for Imported Fabricated Metal Products Purpose / Application ISO 9001:2015 Mandatory (commonly required) Quality management system audit and process control AWS Welder Qualification Mandatory for sanitary welds Ensures welders are trained and tested for TIG/GTAW processes ASME Certification Recommended for certain equipment Pressure vessel / process equipment fabrication standards Mill Test Report (MTR) Mandatory Raw material alloy composition and traceability ASTM A967 (Passivation) Mandatory Corrosion-resistant surface layer restoration Surface Finish Report (Ra ≤ 32) Mandatory for food-contact surfaces Verifies smoothness via profilometer Weld Map / Weld Log with CWI sign-off Mandatory for audit readiness Documents and inspects every weld location Certificate of Conformity (CoC) Mandatory Consolidates all compliance evidence into one audit-ready package FDA (21 CFR) Mandatory for food contact Prevents harmful substance migration into food NSF/ANSI 2 and 51 Mandatory for food equipment Sanitation and material requirements USDA-FSIS Mandatory for meat/poultry/egg equipment Inspection regulations for USDA-inspected facilities 3-A Sanitary Standards Commonly required for dairy/beverage Hygienic design principles for dairy processing lines We review your application to determine which standards apply. A food-processing component requires FDA and NSF compliance. A pressure vessel demands ASME certification. An automotive bracket needs IATF 16949 alignment. Our engineers identify the mandatory standards for your specific product and build the inspection plan around them.
Material Certifications and Full Traceability
Traceability means you can trace every component back to its original material batch. This capability proves essential when quality issues arise, regulators audit your facility, or customers demand documentation. We maintain complete traceability from mill to finished product.
Material traceability documents must be submitted for every batch. Mill certificates accompany every sheet of metal used in the production run. These documents ensure the finished product meets UL-specified standards and prevent voiding of UL listing due to unapproved material substitutions.
We maintain a comprehensive documentation package for each order:
- Mill certificates for every sheet of metal, verifying alloy composition and heat number
- Material test reports documenting mechanical properties and chemical analysis
- Positive Material Identification (PMI) reports confirming alloy grade verification
- Heat traceability records linking each component to its source batch
- Certificate of Conformity consolidating all compliance evidence into one audit-ready package
An EN 10204 3.1 material certificate is an inspection report issued by the manufacturer’s quality department that confirms the material against test results — chemical analysis and mechanical properties tied to the heat number. It is the standard material certificate for industrial procurement when traceability matters.
For full traceability, your request for quotation should explicitly list required records, including the material certificate, EN 10204 type 3.1 (when traceability matters), and PMI (if alloy substitution is a risk). Naming these documents in the RFQ ensures they are included in the quote and not added later via email.
Our spectral analysis equipment verifies material composition at receiving. We compare results against the mill certificate to confirm consistency. Any discrepancy triggers rejection of the entire batch. You receive documented proof that every component originates from certified material that meets your specifications.
Non-Destructive Testing Methods (PT, RT, Pressure Testing)
Non-destructive testing (NDT) verifies component integrity without damaging the part. These methods reveal internal defects that visual inspection cannot detect. We apply NDT techniques according to your specifications and industry requirements.
Liquid Penetrant Testing (PT) detects surface-breaking defects in non-porous materials. Our inspectors apply a colored or fluorescent dye to the surface. The dye seeps into any cracks or porosity. After removing excess dye, we apply a developer that draws the penetrant out. The resulting indication reveals the defect’s location and size. PT proves especially effective for detecting cracks in welds, casting porosity, and surface fatigue.
Radiographic Testing (RT) uses X-rays or gamma rays to examine internal structure. This method produces a permanent image that reveals internal voids, inclusions, and incomplete fusion in welds. RT provides a visual record you can review and archive. We apply RT for critical load-bearing components where internal defects could cause catastrophic failure.
Pressure testing verifies that components withstand their rated operating pressure without leakage. We apply hydrostatic testing for vessels and pipelines, filling the component with water and pressurizing it beyond its rated capacity. We apply pneumatic testing for gas service components, using air or inert gas. Each test follows ASME Boiler and Pressure Vessel Code requirements.
The table below outlines the primary NDT methods we deploy:
Method Defect Detection Best Application Standard Reference Liquid Penetrant (PT) Surface-breaking cracks, porosity Welds, castings, machined surfaces ASTM E165 Radiographic (RT) Internal voids, inclusions, incomplete fusion Critical welds, pressure vessels ASME Section V Ultrasonic (UT) Internal discontinuities, wall thickness Structural steel, plate material ASTM E164 Magnetic Particle (MT) Surface and near-surface flaws Ferromagnetic components ASTM E709 Hydrostatic/Pneumatic Leaks, pressure integrity Vessels, piping, manifolds ASME BPV Code We select the appropriate NDT method based on your component’s function and risk level. A hydraulic manifold requires pressure testing. A structural weld demands RT or UT. A cast housing needs PT to verify surface soundness. Our quality engineers match the testing method to your application’s criticality.
Every NDT procedure follows written instructions. Our technicians hold certifications according to SNT-TC-1A or CP-189 standards. We document all results with photographs and written reports. You receive complete NDT documentation that satisfies audit requirements and gives you confidence in your components’ integrity.
This comprehensive alignment with US and international standards ensures your components meet every regulatory requirement. You receive components that pass inspection, clear customs smoothly, and perform reliably in service.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.Transparency: How You Stay Informed Throughout Production
You never wonder about your order’s status when you work with Qingdao Xuxiangtai. Our transparency protocols keep you informed at every stage. You receive documented evidence of quality, not vague assurances. This visibility eliminates the anxiety that often accompanies overseas sourcing.
Detailed Inspection Reports After Each Stage
You receive a comprehensive inspection report after raw material testing, after in-process checks, and after pre-shipment verification. Each report documents measurements, test results, and compliance status against your specifications. You see exactly what our engineers verified and how your components performed. These reports serve as your permanent quality record for audits and regulatory reviews.
Real-Time Photo and Video Documentation
Pictures provide proof that numbers cannot convey. You receive high-resolution photographs of critical features, weld joints, and surface finishes. For complex assemblies, we record video of trial fit-ups and dimensional verifications. You watch our technicians insert bolts by hand and confirm perfect alignment. This visual evidence gives you confidence that your components meet every requirement before they leave our facility.
Direct Access to Quality Engineers
You communicate directly with the engineers who inspect your components. No intermediaries, no delayed responses. You ask questions about test results, request additional documentation, or discuss tolerance concerns. Our quality team responds promptly with accurate answers. This direct line of communication resolves issues quickly and builds lasting trust between your team and ours.
Transparency is not an afterthought at Xuxiangtai. It is a core principle that guides every inspection protocol we execute.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.The Direct Benefits of Xuxiangtai’s Inspection System for US Purchasing Managers
Your purchasing decisions carry significant weight. Every order you place affects your production schedule, your budget, and your reputation with internal stakeholders. When you write a 1200-word brand-focused English blog for US purchasing managers, you introduce Qingdao Xuxiangtai’s complete quality inspection system for overseas metal manufacturing orders. You cover raw material testing and every subsequent verification stage. The payoff comes in three concrete benefits that directly impact your bottom line.
Reduced Risk of Defects, Returns, and Delays
Defective parts trigger costly return shipments, replacement production runs, and assembly line stoppages. Our multi-stage inspection system prevents these scenarios before they occur. We catch dimensional errors during in-process checks, not after parts arrive at your dock. We verify weld integrity through non-destructive testing while corrections remain inexpensive. This proactive approach eliminates the rework loops that plague fragmented vendor relationships. You receive components that meet specifications the first time.
Smoother Customs Clearance with Complete Documentation
Customs delays stop shipments cold. Missing certificates or incorrect paperwork forces your cargo into warehouse holds. Our documentation package prevents these interruptions:
- Commercial Invoice with correct Incoterms and HS codes
- Packing List detailing every container’s contents
- Certificate of Origin confirming manufacturing location
- Material Test Certificates verifying alloy composition
- Bill of Lading and Importer Security Filing
We pre-file export documents before production completes. This practice cuts one to two days from total transit time. Your freight forwarder picks up and clears customs the same day parts are packed. No idle time at the factory or airport warehouse.
On-Time Delivery Through Proactive Quality Control
Maintaining high-quality standards is essential in metal fabrication. However, rigorous quality control processes can add to the lead time if not integrated efficiently. By optimizing supply chain operations and adopting modern machinery and automation, companies can accelerate processes, improve precision, and ensure consistent quality, thereby reducing lead times and supporting on-time delivery.
Our vertically integrated facility consolidates every process under one roof. You avoid the scheduling conflicts and quality disputes that arise from multi-vendor setups. Early design-for-manufacturability collaboration prevents late-stage changes that carry the highest cost. Direct access to our quality engineers lets you address concerns immediately. Small issues never become large ones. Your delivery date stays protected.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.
This complete quality inspection system represents more than process—it protects your business interests. You gain a reliable partner ensuring quality, compliance, and timely delivery at every production stage. Contact Qingdao Xuxiangtai today for a detailed walkthrough or to discuss your specific project requirements.
Submit your drawings and quality requirements for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
FAQ
Q: Do you provide material certifications?
A: Yes. We supply spectral analysis reports and full material traceability for every batch.Q: Can I receive inspection reports after each stage?
A: Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection.Q: How do you handle export compliance for US customs?
A: We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance.FAQ
Do you provide material certifications?
Yes. We supply spectral analysis reports and full material traceability for every batch. Each certificate documents alloy composition, heat numbers, and mechanical properties. You receive complete verification before shipment.
Can I receive inspection reports after each stage?
Absolutely. We issue detailed reports with photo and video documentation after raw material testing, in-process checks, and pre-shipment inspection. You track quality progress at every milestone.
How do you handle export compliance for US customs?
We prepare complete documentation, including material certificates and test results, ensuring smooth customs clearance. Our team verifies all paperwork against current US import regulations before your shipment departs.
Submit your drawings and quality requirements today for a detailed quotation. Our engineers will review your specifications and propose a tailored inspection plan.
See Also
Avoid Selecting Incorrect Aluminum Casting Methods Forever
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.